Metal forming in Mexico
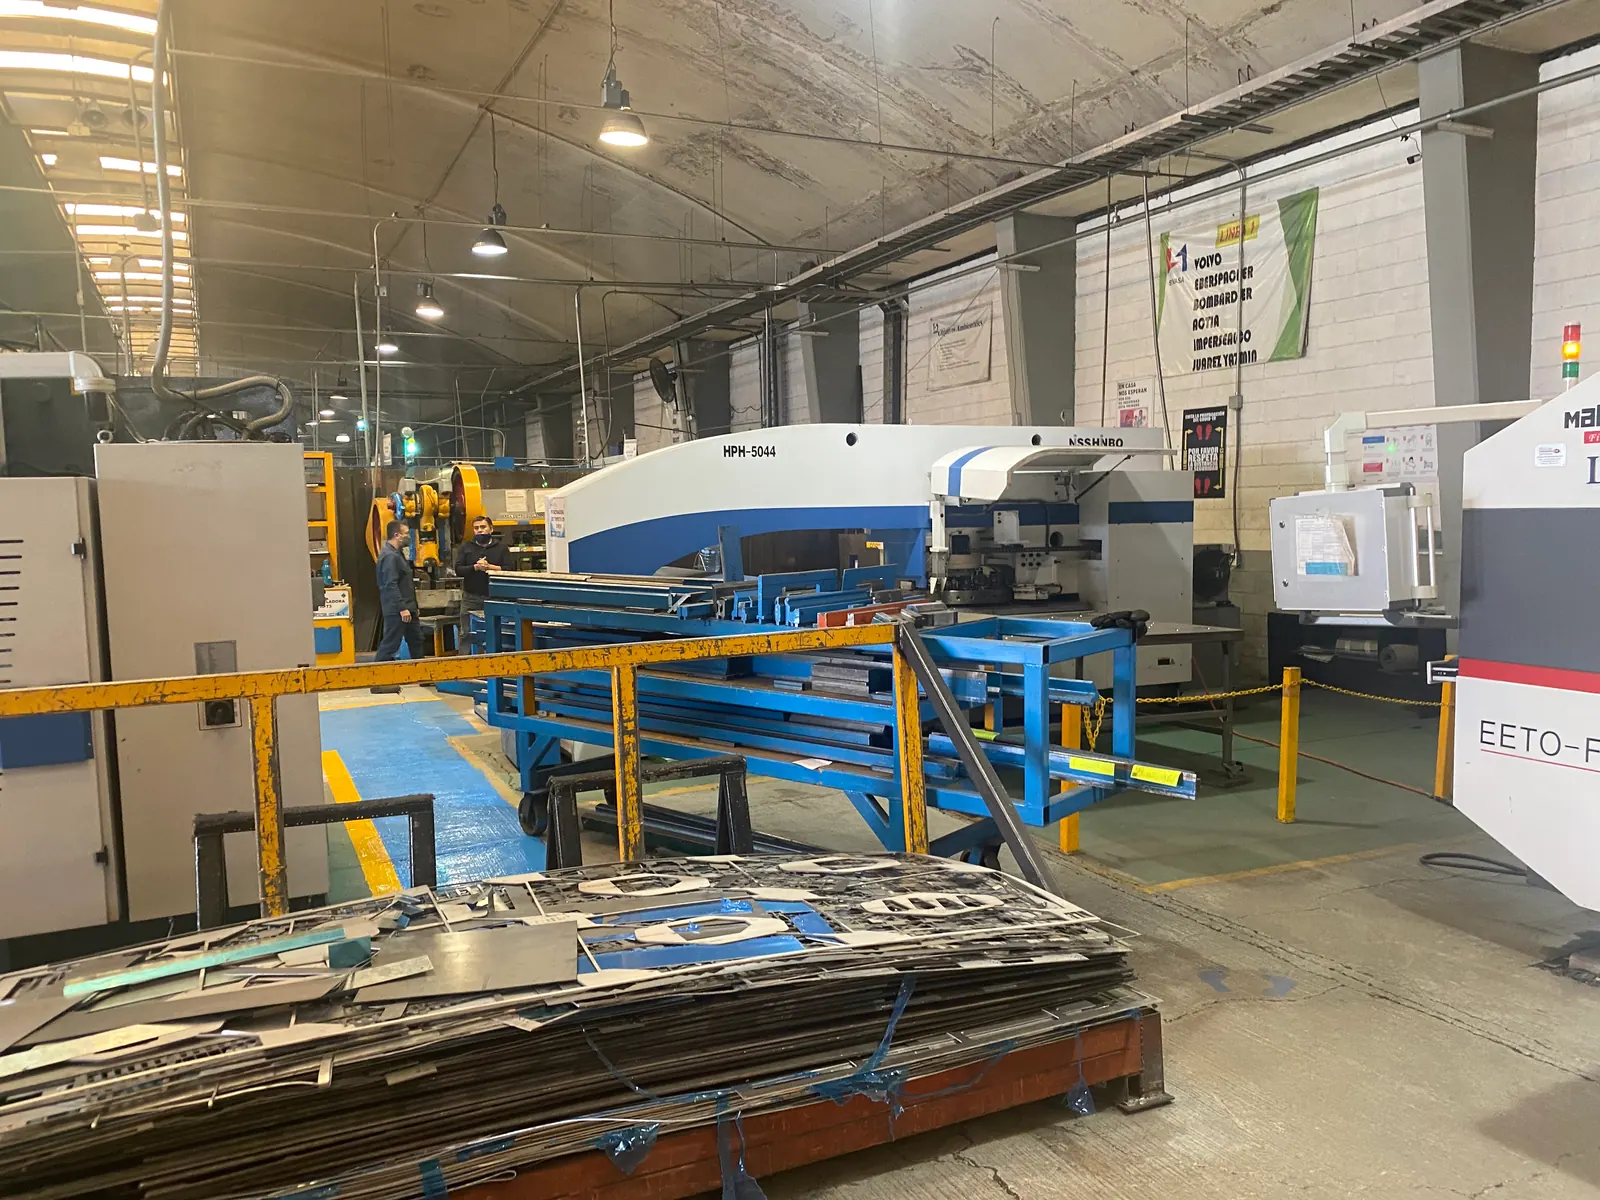
Bend radius and sequence decide whether the finished part fits. We work back from assembly fit to the flat pattern, tooling, and inspection plan.
Bend order and assembly fit on Mexico formed parts
Bend order and assembly fit
A small change in bend radius can move every hole and flange that follows it. We work backward from assembly fit to the flat pattern, grain direction, relief, and bend order. The proposed press brake, tooling, and inspection route are verified with the assigned Mexico partner for the part.
- Material gaugereviewed per part
- Bend tolerancechecked against drawing
- Bend lengthverified with selected plant
- Process controlsset in quality plan
Measurement and traceability agreed on Mexico bends
Bend inspection and traceability
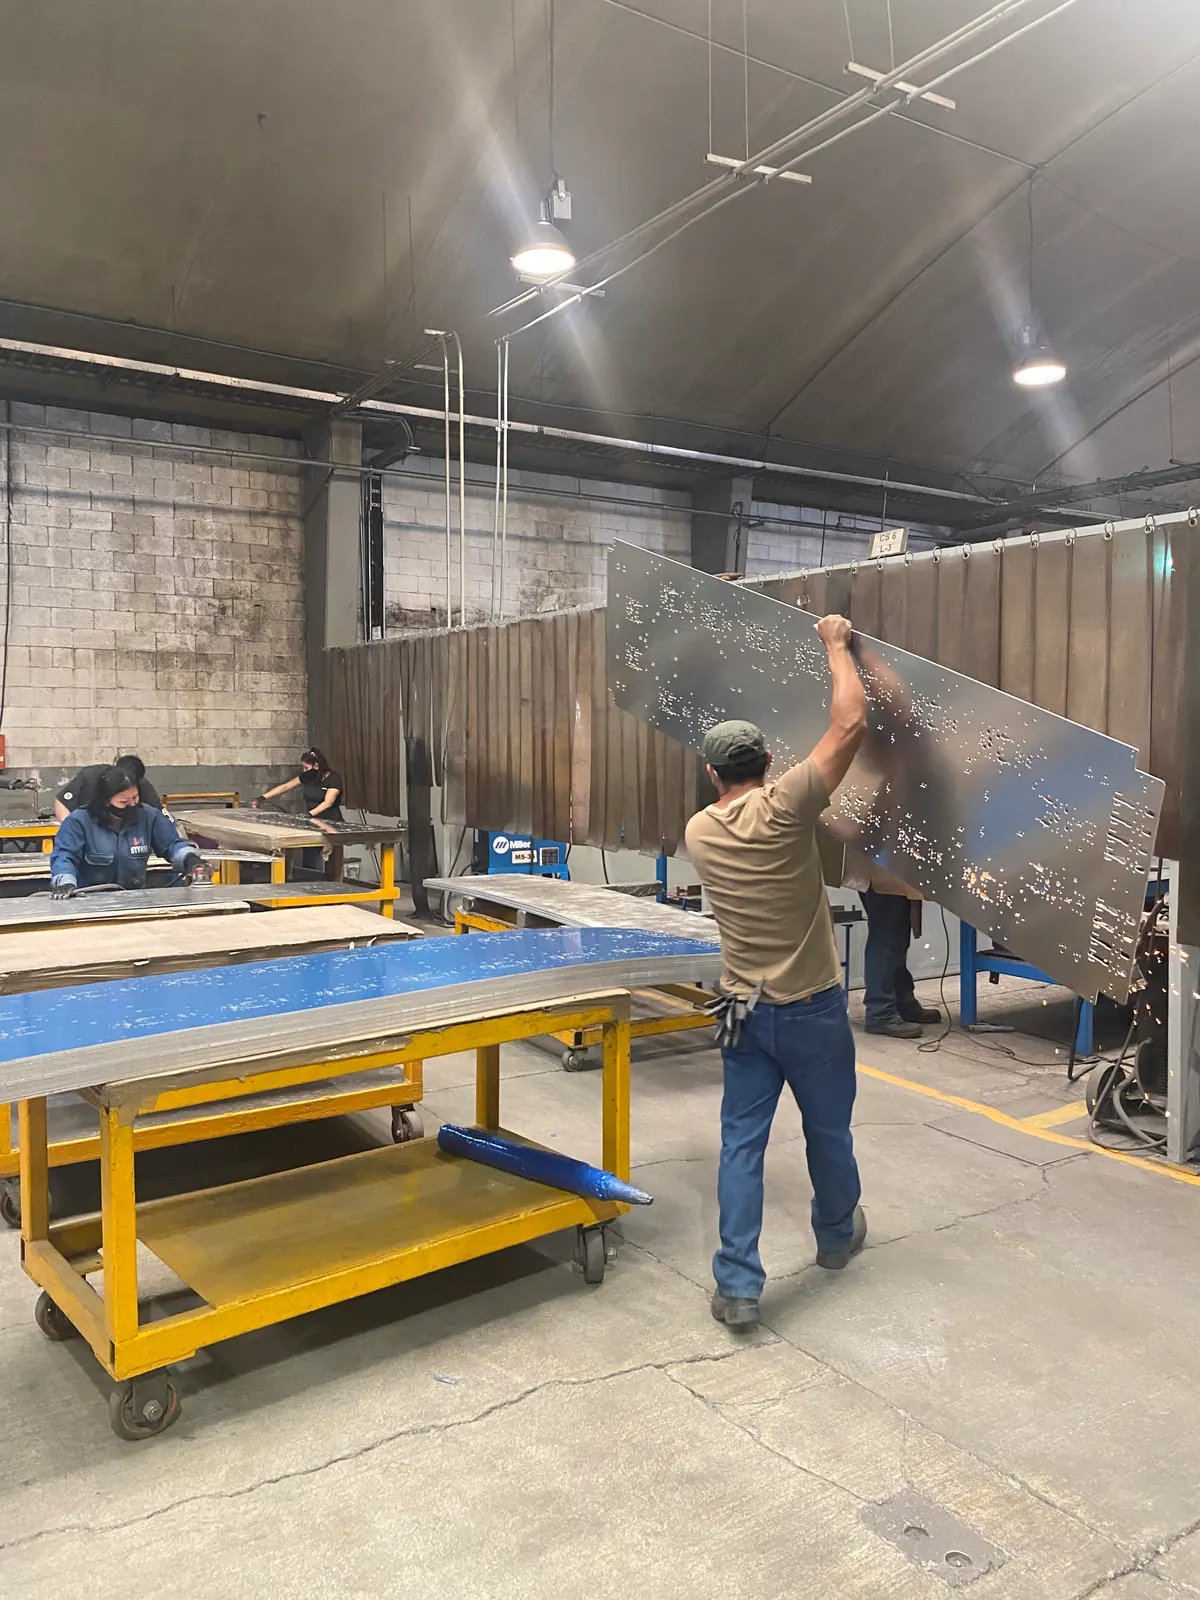
Statistical process control, lot traceability, and third-party inspection at origin are specified when the part and selected production site call for them. A dimensional report, visual inspection, material certification, and PPAP documentation are agreed in the quality package before quoting rather than assumed for every shipment.
-
Statistical process control Statistical process control, lot traceability, and third-party inspection at origin are specified when the part and selected production site call for them.
-
Dimensional report A dimensional report, visual inspection, material certification, and PPAP documentation are agreed in the quality package before quoting rather than assumed for every shipment.
-
PPAP documentation A dimensional report, visual inspection, material certification, and PPAP documentation are agreed in the quality package before quoting rather than assumed for every shipment.
Gauge and bend limits confirmed for a Mexico plant
Gauge, bend length, and bend-angle limits
Gauge, bend length, and tolerance get confirmed against material and bend count at quoting. The requirements below are checked against the assigned partner plant and tooling before any program is accepted. Heavier plate is assessed individually.
- Material gauge
- Set by material, geometry, and selected equipment
- Bend length
- Matched to press brake and tooling
- Bend angle tolerance
- Set from drawing, material, and springback
- Bend-to-bend tolerance
- Controlled by setup and inspection plan
- Tighter tolerance review
- Feasibility checked on the critical features
Materials
Bend radius and grain direction by material gauge
Steel, stainless steel, and aluminum are evaluated for forming. Gauge, bend radius, relief, and grain direction factor into flat pattern development. Powder coating, anodizing, zinc plating, chromate conversion, and wet paint are finishes to review, with availability and compatibility confirmed for the selected partner plant and part.
Example parts
Chassis, guards, and formed brackets
Chassis, enclosures, and brackets for electronics, plus frames, guards, and mounting plates for industrial equipment, are examples to assess, alongside brackets, heat shields, and structural panels for automotive volume programs. Hardware housings that proceed to welding or assembly after bend approval also run through this process.
-
Chassis, enclosures, and brackets
for electronics
-
Frames, guards, and mounting plates
for industrial equipment
-
Brackets, heat shields, and structural panels
for automotive volume programs
-
Hardware housings
welding or assembly after bend approval
From model to approved bends on a Mexico program
From model to approved bends
Part files, material, gauge, and annual volume get reviewed before quoting forming, finishing, freight, and customs. Once the order is placed, the flat pattern and first-article schedule get confirmed, samples are formed for sign-off, and production runs under process controls before shipment to the receiving dock.
-
Review model, material, and gauge
Part files, material, gauge, and annual volume
-
Confirm quote and production plan
forming, finishing, freight, and customs
-
Develop flat pattern and first article
the flat pattern and first-article schedule get confirmed
-
Run forming under agreed process controls
production runs under process controls
-
Inspect and coordinate shipment
shipment to the receiving dock
Metal forming in Mexico, common buyer questions
Frequently asked questions
Can cutting and forming run together?
Send the flat pattern and bend requirements so we can confirm whether cutting and forming can run at the same site. We quote the cut and the bends together once we review the model, material, gauge, bend sequence, and required finish.
What forming tolerances should a drawing specify?
Specify the tolerances required for part function and assembly fit. We check bend angle, bend-to-bend dimensions, gauge, and length against the material, tooling, and assigned partner plant before committing to a tolerance in the quote.
How are gauge and bend-length limits set?
Material, part length, tooling, and bend count determine which press brake fits. We verify the proposed plant's equipment against your drawing before the quote states gauge and length limits. Plate parts get a separate feasibility review.
Can we transfer an existing formed part?
Yes. We compare your current flat pattern, material, tooling, and supplier quote with a proposed Mexico route. The written quote compares landed cost and lead time and sets first-article approval before you move production.
Send a flat pattern for press brake work in Mexico
Quote a formed part
Send the model, material, gauge, and annual volume, and we will review bend feasibility and the cut-and-form route.